
Table of Contents
Starting point — the core production problem
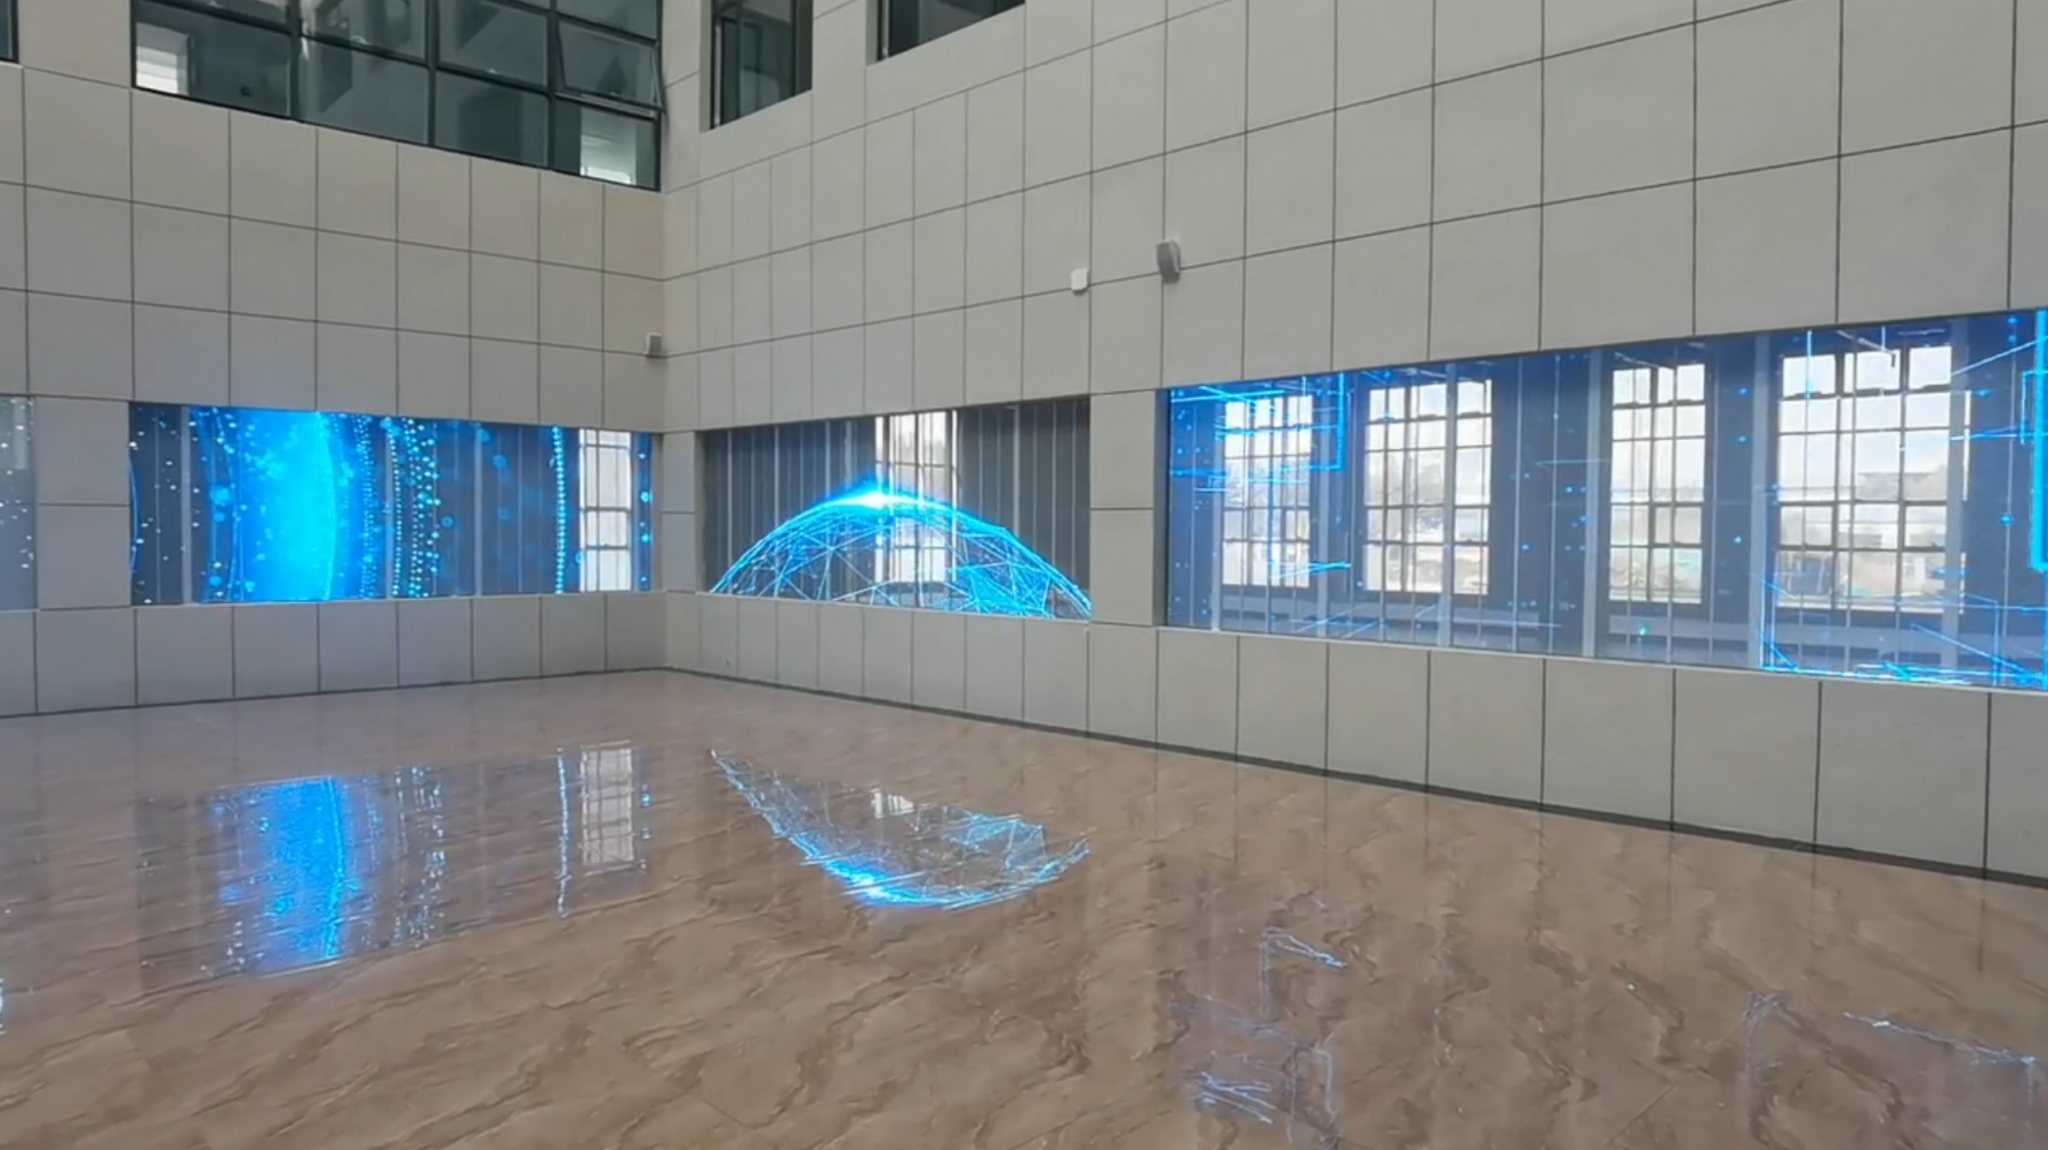
Manufacturers often confront the same set of blockers: ambiguous specifications, inconsistent supplier quality, and thermal or optical failures discovered only after production ramps. Those issues force costly reworks and missed delivery windows; even a campaign as simple as a retail window install or a led poster display can become a project risk if early choices are wrong. A problem-driven approach focuses on eliminating these failure modes before tooling begins.
Pinpointing failure modes
Start by listing measurable risks: mechanical tolerances that prevent module seating, heat-dissipation gaps that shorten LED life, supplier part swaps that change color characteristics, and insufficient EMC testing that causes field interference. Treat each risk as a requirement item with an owner and an acceptance test. That shifts conversations from vague assurances to demonstrable checkpoints.
Engineering responses that reduce rework
Design for manufacturability (DFM) is not optional. Require thermal simulation results tied to specific ambient conditions, specify connector retention forces, and lock down color calibration targets with Delta E tolerances. Use desktop prototypes to validate assembly jigs and create a pilot run of 10–50 units before committing to mass tooling. Standardize burn-in and vibration tests so they are repeatable across contract manufacturers.

Experience, evidence and a real-world anchor
Years of factory audits and production line observations show the same pattern: projects that document test gates and enforce them hit shipment targets and warranty goals. At CES in Las Vegas, companies demonstrated modular formats that highlight how early verification speeds adoption; one clear example on show was the Foldable poster led display, which exposed integration pitfalls that are easy to miss on paper. Use test reports, compliance certificates, and field failure data as your evidence set — assemble them into a single dossier before provider selection.
Common pitfalls and how to avoid them
Don’t outsource specification control. Suppliers will optimize to bid constraints, not long-term lifetime, unless expectations are explicit. Avoid last-minute component substitutions by requiring change approvals tied to requalification. Resist the impulse to skip environmental stress screening to save time; early screening catches infant mortality that becomes expensive recalls. Finally, validate firmware update procedures and secure boot processes before units ship.
Operational milestones for a clean ramp
Define milestones that gate spend: specification freeze, DFM signoff, prototype validation, pilot production with full test logs, and a controlled ramp with inline quality sampling. Assign responsibility for each milestone and require pass/fail criteria that are objective. Track supplier KPIs — on-time delivery, first-pass yield, and field return rate — and tie payments or future orders to them.
Bringing the solution to market
Clear specifications, rigorous pilot runs, and documented test evidence convert risky projects into repeatable programs. That practical sequence aligns engineering diligence with procurement and operations so production meets specification and schedule — a pattern consistently implemented by partners such as HDC.
